Line heating technology
When the line heater is controlling the heating process, they do so by observing the colour of the material, so there is a lack of consistency and control. This can often result in the hardening of the material due to excessive temperatures, destroying its useful properties.
IACS (International Association of Classification Societies Ltd) standard No.47 publication gives a mandatory maximum steel surface temperature of 650 ºC when cooling down with water. However, heating above 727°C with subsequent quenching causes the forming of Martensite which in turn makes the material brittle and have a low ductility.
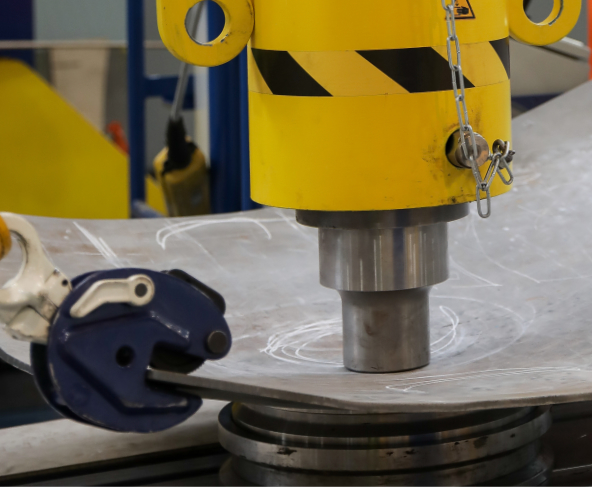
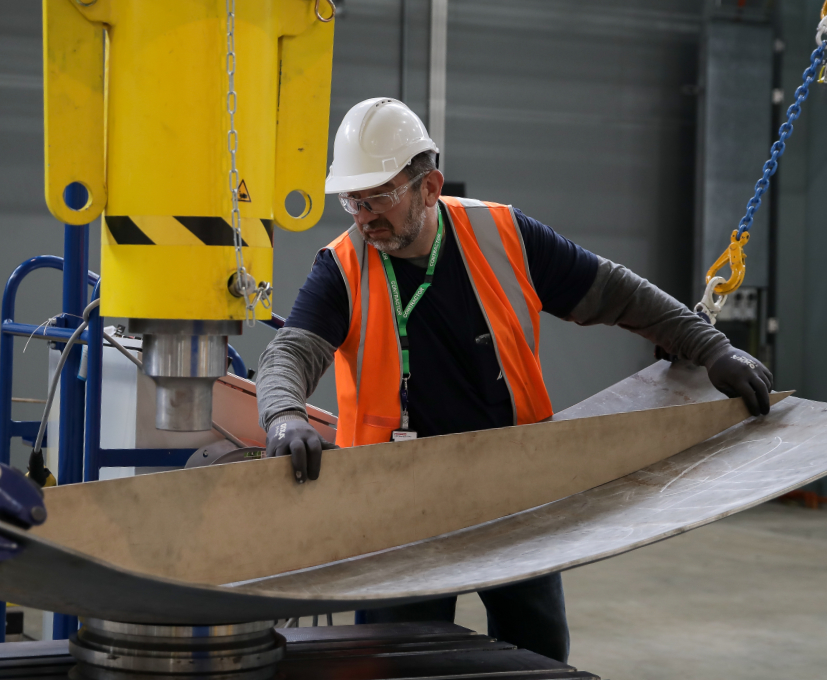
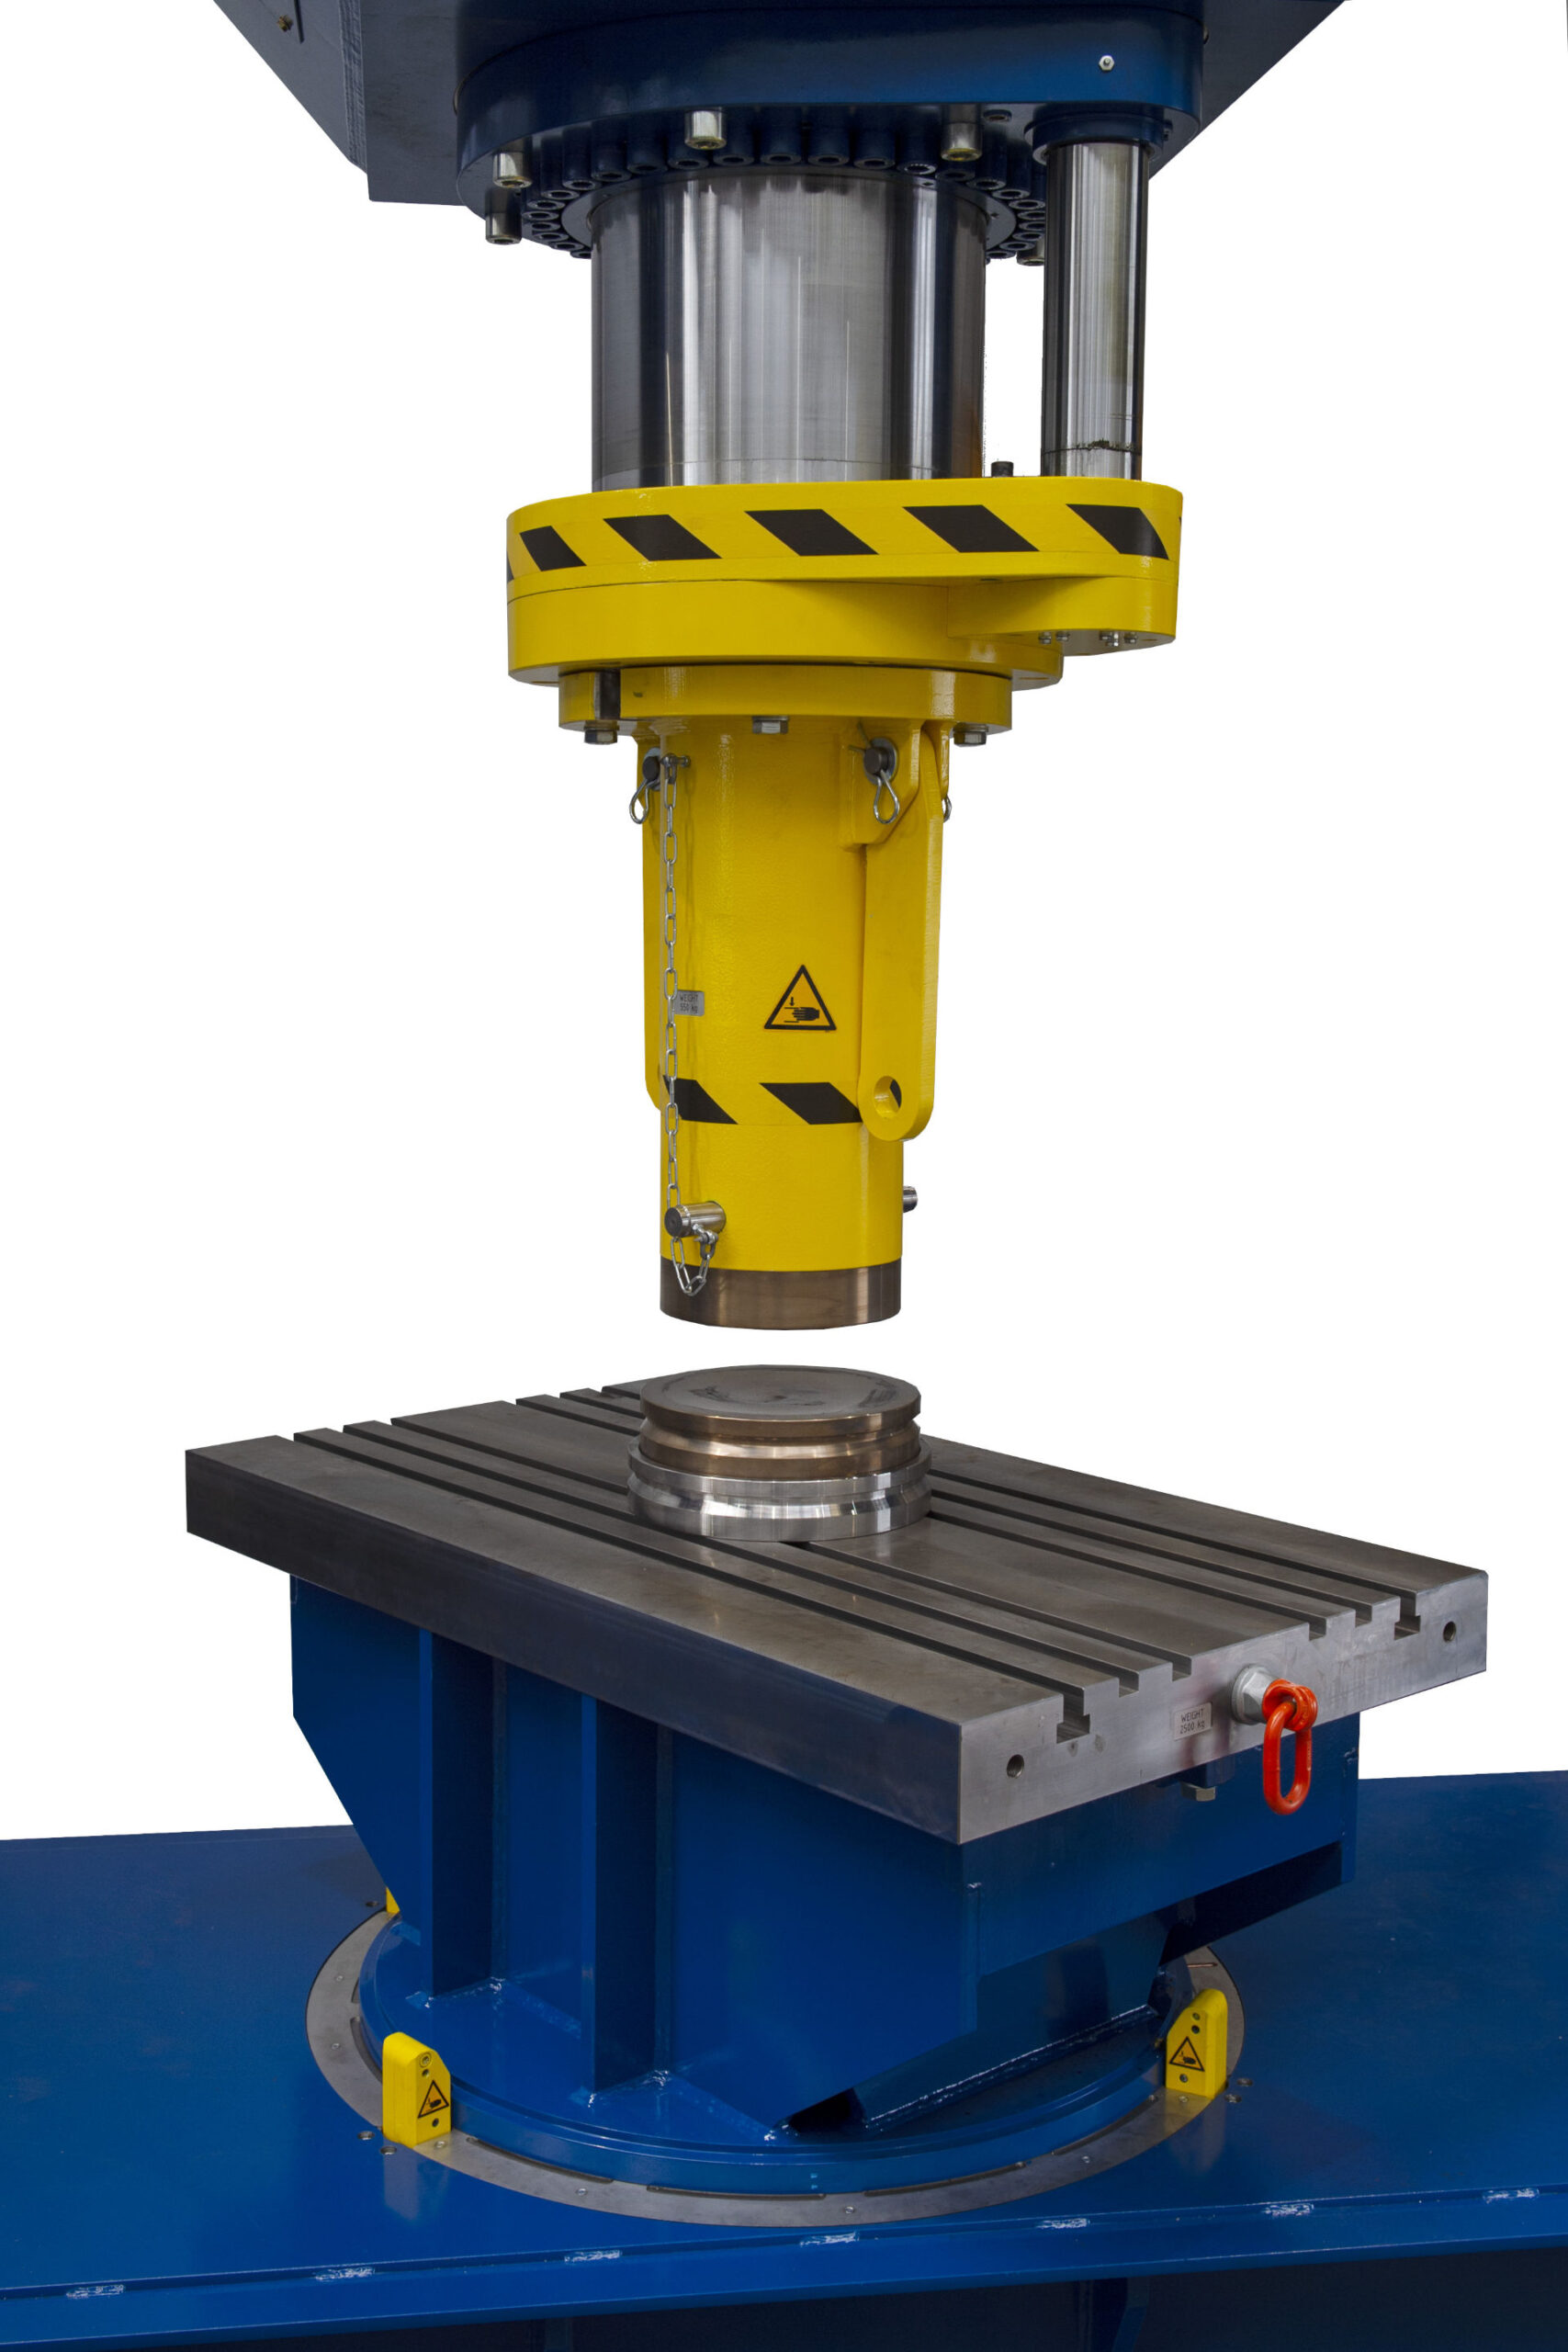
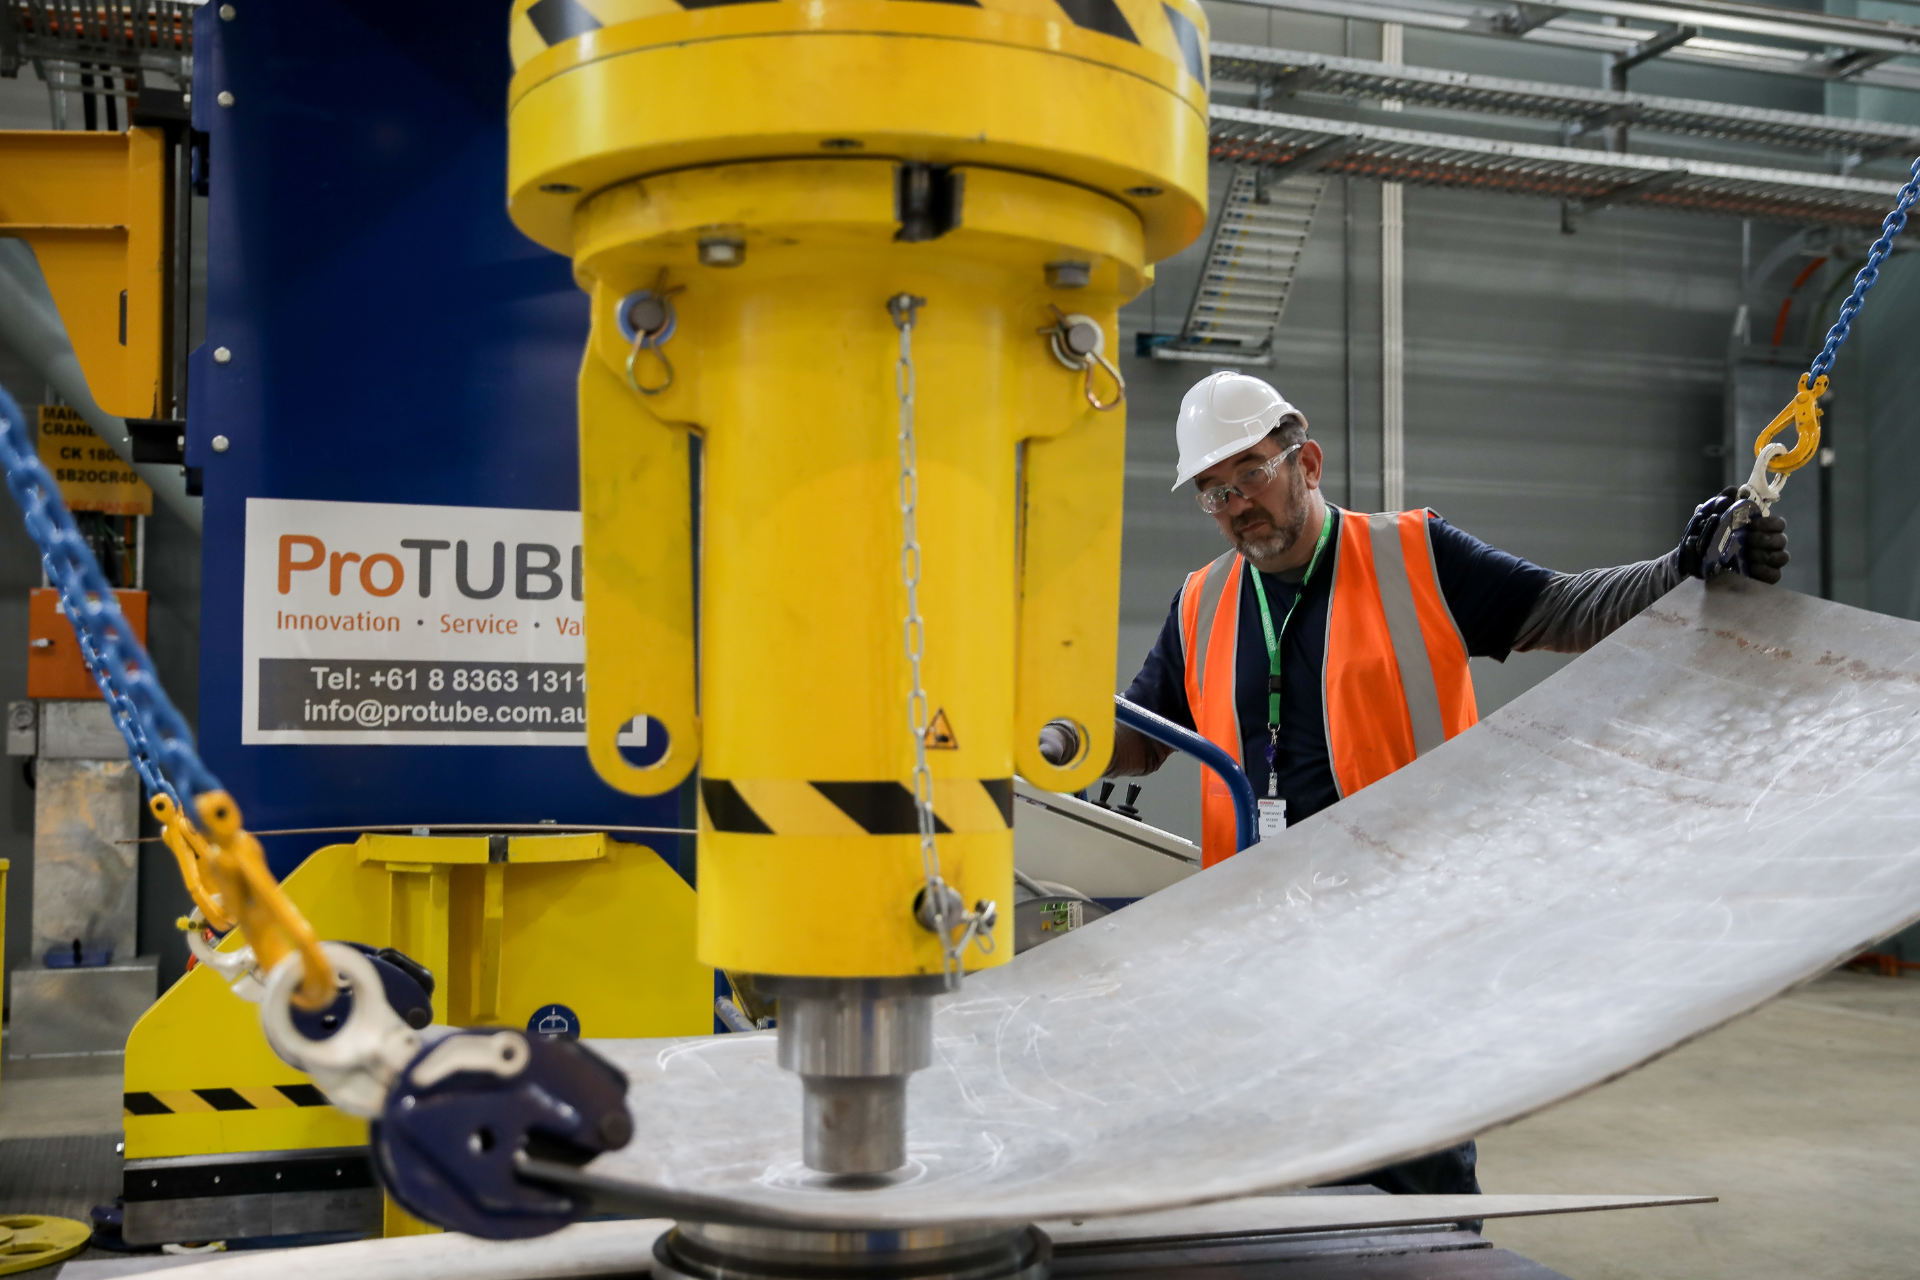
An additional benefit in switching from line heating to cold forming, is the production efficiency. For example, a saddle-shaped panel requires 1.5 hours for cold forming on a Nieland press but takes two days at least with line heating.
Moreover, training a line heater will take 5-10 years whereas cold forming takes an initial 3 months, followed by 1-2 years of practice. To be short, the ROI for cold forming in itself will enable Nieland to surpass line heating in the next decennium.